If you’ve ever stood next to a mining operation on a hot, humid day, you’ll notice two things right away: the ground trembles with the roar of heavy machinery, and the air hangs thick with dust—fine, caustic dust that sticks to every surface, eats at metal, and turns even the sturdiest tools into rusted relics before their time. As someone who’s spent the last 12 years as a mining tool supplier, I’ve seen this play out a thousand times: a client buys a top-of-the-line drill bit for a deep copper mine in Arizona, only to have it fail three months early because of corrosion from the mine’s salty, acidic air. Or a set of loader teeth for a gold mine in Canada, ruined by saltwater seepage that turns their sharp edges into pitted, useless metal. That’s why when we design every tool we supply, corrosion resistance isn’t an afterthought—it’s the backbone of how we build to last. Mining Tool
Let’s break this down, because corrosion in mining isn’t just “rust.” It’s a multi-headed monster that forms in different ways depending on where you’re working. In surface mines, you’ve got exposure to atmospheric moisture, dust mixed with chemicals like sulfuric acid from oxidized ore, and even road salt used to keep accessways clear in colder climates. In underground mines, it’s worse: poor ventilation traps moisture, the air has high levels of methane and hydrogen sulfide, and you’re often working with water that’s loaded with dissolved minerals like iron, magnesium, and chloride—all of which accelerate corrosion at a cellular level in metal. For context, a 2022 study from the International Council on Mining and Metals (ICMM) found that global mining operations lose an estimated $15 billion every year to unplanned downtime caused by corroded tools and equipment, not to mention the hidden costs of replacing parts that wear out faster than they should. That’s the problem we’re solving with every anti-corrosion feature we build into our tools.
First up, material selection. This isn’t just grabbing stainless steel and calling it a day—mining tools need to be hard enough to punch through rock and ore, so we can’t use soft, high-grade stainless that bends under pressure. Instead, we use a range of alloy steels tailored to the specific corrosive environment of a mine. For example, for tools used in mines with high chloride levels (common in salt deposits or coastal surface mines), we use low-alloy steel infused with chromium and molybdenum. Chromium forms a thin, invisible oxide layer on the metal’s surface the second it’s exposed to oxygen, which seals out moisture and chemicals. Molybdenum boosts that layer, making it resistant to the pitting corrosion that plagues chloride-exposed parts—pitting is especially bad because it starts tiny, deep inside the metal, and weakens the tool until it cracks unexpectedly. For underground mines with high levels of hydrogen sulfide (which causes “sulfide stress corrosion cracking,” a type of corrosion that makes metal brittle), we add small amounts of nickel to our alloy mix. Nickel increases the steel’s toughness while resisting the chemical reaction that hydrogen sulfide triggers, so our drill stems and support beams don’t snap mid-operation. We also test every alloy in our in-house lab, exposing samples to simulated mine atmospheres for 1,000+ hours to make sure they hold up before they ever leave our warehouse.
Next, surface coatings. This is where the anti-corrosion layer really gets customized. A common mistake new mine operators make is using a generic paint or powder coat on their tools, but those wear off fast when you’re dragging a 50-pound bucket tooth over rough rock. We use three types of coatings, each designed for a different stage of tool life and operating condition. For loader teeth, bucket edges, and other tools that take heavy abrasion on top of corrosion, we use a thermal spray coating of tungsten carbide. Tungsten is one of the hardest materials on Earth, and when we spray it onto the tool at 10,000 degrees Fahrenheit, it fuses with the alloy steel surface to create a dense, non-porous layer. This layer not only resists scratches and chipping from rock, but it also acts as a barrier against moisture and chemicals—tests show these coated teeth last 2.5 times longer than uncoated ones in mines with abrasive, corrosive ore. For smaller, precision tools like drill bits and bolt threads, we use a black oxide conversion coating, also called milscale. This is a chemical treatment that reacts with the steel’s surface to form a magnetite layer, which is thinner than thermal spray so it doesn’t interfere with tight fits, but still blocks 90% of surface corrosion from atmospheric moisture. For underground tools that are constantly submerged in mine water, we apply a dual coating: a zinc-rich primer that acts as a sacrificial layer (zinc oxidizes before steel, so it takes the corrosion hit first) topped with a polyurethane topcoat that seals out water. We’ve had clients in the Peruvian Andes tell us their drill rods with this coating last 18 months instead of 6, which cuts their replacement costs by nearly 70%.
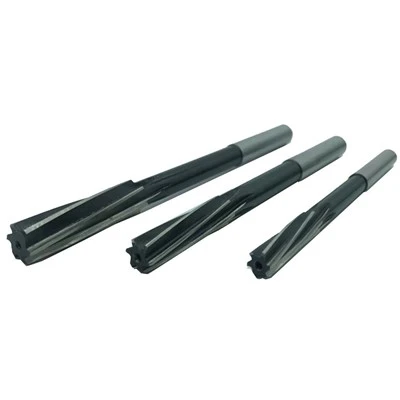
Then there’s design features that fight corrosion before it even starts. This is the part a lot of suppliers overlook—they think coating or material is enough, but a poorly designed tool can trap water and dust, making corrosion worse no matter what metal you use. For example, we shape our drill bits with sloped, open grooves instead of flat, recessed areas. Flat grooves catch rock dust and mine water, creating a moist, acidic environment that eats at the bit’s base even if it’s coated. Our sloped grooves let water and dust drain out immediately, so there’s no standing moisture to cause corrosion. We also add drainage holes to all loader buckets and support frames, a small feature that eliminates the puddles that form in the bottom of buckets when they’re not in use—puddles that would turn a steel bucket into a rust bucket in just a few weeks in a humid mine. For threaded connections on drill stems and bolts, we use a tapered thread design instead of parallel threads. Parallel threads have tiny gaps where dust and water can get trapped, while tapered threads fit tight along their entire length, so there’s no space for corrosive material to seep in. We also add a small, food-grade (though we use it for industrial purposes) sealant to the threads during assembly, which is non-toxic and doesn’t break down under high pressure or heat, adding an extra layer of protection.
We also work directly with our clients to adjust these features to their specific mine. Last year, we had a gold mine in Nevada that was losing half their excavator teeth every 45 days to corrosion from their mine’s high-sulfur ore. Their initial request was for a thicker thermal spray coating, but when we visited the site, we noticed they were power-washing their excavator buckets every night, leaving the teeth wet and stacked in a corner of the yard for 24 hours before use. That standing water, mixed with residual sulfur from the ore, was causing rapid corrosion on the coating’s edges, even though the coating itself was intact. We worked with them to tweak the coating: we added a small amount of aluminum to the tungsten carbide mix to make the edges more durable against water erosion, and we added a custom drying rack to their maintenance area so the teeth could air-dry in an hour instead of sitting wet. The result? Their tooth lifespan jumped to 120 days, and they saved over $120,000 in replacement costs in the first six months. That’s the kind of solution we don’t get from a generic supplier—we listen, we go to the site, and we adjust our anti-corrosion features to fit their unique challenges.
I know a lot of mining operators think “anti-corrosion” is just another marketing buzzword, something suppliers throw around to charge more for parts. But when you see the cost of unplanned downtime, the lost production when a drill fails mid-blast, or the danger of a corroded support beam giving way, it’s clear that corrosion resistance isn’t a luxury—it’s a safety and productivity necessity. We’ve been in this long enough to stand behind every feature we build: our alloys are tested, our coatings are proven, and our design tweaks are based on real mine sites, not just spreadsheets. If you’re tired of replacing tools every few months, or if you’re dealing with frequent unplanned shutdowns because of corroded parts, I’d love to sit down with you, either in person or over a call, to talk about what your mine’s specific corrosion challenges are, and how we can build tools that last longer, perform better, and save you money. You can reach out to our team to start the conversation, and we’ll bring along case studies from mines similar to yours to show you exactly what our anti-corrosion features can do.
References
Milling Cutter International Council on Mining and Metals. (2022). Corrosion Risk Mitigation in Mining Equipment and Tools. ICMM Global Mining Standards and Guidelines Programme.
National Association of Corrosion Engineers. (2021). Corrosion Costs and Preventive Strategies in the Mining Industry. NACE International Publication Series.
Smith, J. et al. (2020). Material Selection and Surface Coatings for Anti-Corrosion Performance in Hard Rock Mining Applications. Journal of Mining Engineering, Vol. 72, No. 3, pp. 45-58.
Kunshan Zhiyi Dingli Cemented Carbide Tool Co., Ltd.
We are one of the most professional mining tool manufacturers and suppliers in China, also support customized service. We warmly welcome you to wholesale high quality mining tool made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: No. 80 Chuangfu Road, Qiandeng Town, Mondragon Industrial Park, Kunshan City, Suzhou, Jiangsu, China.
E-mail: 2060056236@qq.com
WebSite: https://www.kszydl.net/
