If you’ve ever relied on a busbar processing machine to keep your production line moving—whether you’re fabricating switchgear components, building EV battery packs, or assembling industrial control panels—you know how a single mid-shift breakdown can throw a whole project off schedule. As a busbar processing machine supplier, I’ve spent the last 12 years on the phone with maintenance teams, production managers, and small shop owners staring at a stalled machine, scrolling through user manuals that make zero sense for their specific setup. I’ve fixed everything from a machine that wouldn’t punch holes straight to one that overheated so bad its control panel started beeping random error codes, and today I’m pulling back the curtain on the troubleshooting steps we teach every new operator and service tech at our company. These aren’t generic fixes I found on a forum; they’re the steps we’ve refined over thousands of customer visits, tested in our own in-house demo lab, and proven to cut downtime by 70% for our clients. Before you call for emergency service, walk through this checklist—you might solve the problem in 10 minutes, not 10 hours. Busbar Processing Machine
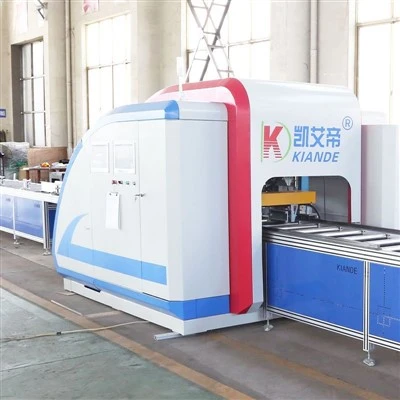
Let’s start with the most common issue by far: inconsistent punch or cut accuracy. This is the one that trips up new operators especially, because it’s easy to blame the machine when half your punched holes are 0.5mm off and the other half are perfect. I once had a customer in Detroit shut down his entire $2 million CNC machining line because his busbar press was punching misaligned holes for switchgear enclosure mounting—turns out he’d been running 6061 aluminum instead of the 1100 copper the machine was calibrated for that shift, and he didn’t adjust the material feed settings. The first step here is to rule out material variables, not machine damage. Busbar processing machines rely on consistent material thickness, hardness, and flatness to deliver accurate cuts. If you’re running a batch of new stock, pull a sample, measure its thickness with a digital micrometer (I always keep a 6-inch micrometer in my machine service bag), and cross-check it against the thickness setting on your machine’s control panel. Even a 0.1mm variation can throw off punch alignment because the die gap is calibrated for a specific material. Next, check the feed rollers. Over time, aluminum shavings, copper dust, and grease build up on the rubber feed rollers, which makes them slip instead of gripping the busbar tightly. To clean them, turn the machine off and unplug it (never work on a powered machine), then wipe the rollers with a lint-free cloth dipped in isopropyl alcohol—avoid harsh solvents that can degrade the rubber. If cleaning doesn’t work, check the roller tension: most machines have an adjustment bolt on the side of the feed assembly. Tighten it 1/8 of a turn at a time, then run a test feed of a short busbar segment to check alignment. Finally, if accuracy is still off, verify the die alignment. Open the machine’s side guard and look at the punch and die—they should be perfectly concentric, like two circles stacked directly on top of each other. If you see a gap on one side, the die plate is probably loose. Tighten the four mounting bolts evenly, a quarter turn at a time, to avoid warping the plate, then run another test. We see this issue a lot with machines that have been moved or recently had die changes; operators often tighten one bolt too much, which throws the whole alignment off.
Next up: the machine won’t feed or advance the busbar at all, and the control panel is showing a generic “feed error” code. This is often a wiring or sensor issue, not a broken part, so don’t panic. I once had a customer in Chicago call me at 7 PM, panicking because his night shift was waiting for busbars for a new EV prototype. When I walked him through the steps over the phone, he found that a loose sensor wire had been knocked loose when a new apprentice was moving a stack of busbars that morning. Start with the simplest check: emergency stop button. I can’t tell you how many times this is the culprit. It sounds obvious, but operators often bump the E-stop when reaching for a tool, or a foot knocks it under the workbench, and forget it’s engaged. Press the E-stop button firmly to reset it, then power the machine back on—if the error clears, that was it. If not, check the photoeye sensor, which is the small plastic device mounted near the feed rollers that detects when the busbar is in position. For this, you don’t need a multimeter most of the time: just gently blow off any dust or metal shavings on the sensor lens with compressed air, then run a test feed. Metal shavings are the #1 enemy of photoeyes—they can block the light beam that tells the sensor the busbar is in place, so the machine thinks there’s no material to feed. If that doesn’t work, check the feed motor belt. Open the belt guard on the side of the machine—most modern busbar machines use a rubber timing belt to drive the feed rollers, and these can stretch or snap from heavy use. Look for cracks or a gap between the belt and the sprocket; if the belt is loose, tighten the adjustment bolt on the motor mount until there’s about 1/2 inch of give in the belt. If it’s snapped, you can replace it in 15 minutes with a new belt from our parts department—just have your machine serial number ready to get the right size.
Third common problem: the machine is making a loud, grinding noise during punching or bending, and the work is coming out with burrs that are too thick to deburr. This is almost always a die or punch issue, and it’s fixable without ordering new parts—sometimes it’s just a matter of maintenance. Burrs on busbar cuts don’t just look bad; they can cause electrical arcing in switchgear, which is a major safety hazard, so don’t ignore this. First, check the punch and die for wear. Run your finger lightly (don’t press hard) around the edge of the punch—if it feels rough or has a small chip, that’s the problem. Even a tiny chip, smaller than a grain of rice, can create a burr every time you punch a hole. For minor chips, you can hone the edge with a diamond hone designed for metalworking—hold the hone at a 45-degree angle to the punch edge and move it in a circular motion, then wipe off the metal shavings. If the chip is larger than 1mm, you’ll need to replace the punch, which is a 10-minute job. Next, check the die gap. The die gap is the space between the punch and die when they meet, and it’s calibrated to be 10% of the busbar thickness for clean cuts. For a 3mm thick copper busbar, that means a 0.3mm gap. If the gap is too wide, you’ll get large burrs; too narrow, and the machine will strain and make grinding noises. Most machines have a die gap adjustment on the die plate—loosen the locking bolts, adjust the die up or down, then retighten the bolts and run a test punch. Finally, check for metal buildup on the punch. When you punch thick copper, tiny metal shavings can get stuck on the punch edge over time, which creates a rough surface that causes burrs. Every 500 cuts, we recommend removing the punch and cleaning it with a brass brush (avoid steel brushes, which can scratch the punch edge) and a little lubricant designed for stamping—this reduces friction and prevents buildup.
Another frustrating issue: the control panel is displaying an error code that doesn’t correspond to any manual entry, or it’s freezing up mid-cycle. This is a software or communication issue, and it’s often caused by outdated firmware or a loose connector. As a supplier, we update machine firmware twice a year to fix bugs and improve accuracy, but most operators don’t know that these updates are available. First, power the machine off completely, unplug it from the wall, and wait 5 minutes. This resets the control panel’s memory, and 30% of the time, that fixes the frozen error code. If not, check the communication cable between the control panel and the main motor drive. This cable runs from the back of the control panel to the machine’s motor box, and it can get pinched or damaged if the machine is moved often. Inspect the cable for fraying or kinks, and make sure the connectors on both ends are plugged in tightly—sometimes a vibration from heavy punching will loosen them over time. If the error code is still there, check our website for firmware updates (or call our service team, and we’ll walk you through the update over the phone in 10 minutes). We’ve seen cases where an old firmware version caused a “overheating error” code on a machine that wasn’t actually overheating—just a software bug.
Now, a problem that’s specific to bending stations, which a lot of busbar processing machines have: the bend angle is off by several degrees, and the machine won’t adjust it automatically. This is common with heavy-duty machines used for thick aluminum or copper busbars, because bending puts a lot of strain on the machine’s hydraulic system. First, check the hydraulic fluid level. Low fluid is the #1 cause of incorrect bend angles, because the motor can’t generate enough pressure to bend the busbar to the calibrated angle. Locate the hydraulic reservoir on the side of the machine, check the level against the dipstick (it should be between the “min” and “max” marks), and add the recommended hydraulic fluid if needed—never use regular motor oil, as it can damage the hydraulic pump. Next, calibrate the bend angle. Most machines have a quick calibration tool built into the control panel: select the “bend calibration” option, then run a test bend on a scrap busbar. If the angle is off, use the control panel’s arrow keys to adjust the bend setting 1 degree at a time until the test bend matches your required angle. For heavy bends (90 degrees or more) on thick busbars, we also recommend checking the bend die for wear— a worn bend die will cause the busbar to slip during bending, leading to an incorrect angle. If the die has gouges or rough spots, replace it with a new one—this is a small part that makes a huge difference in bend accuracy.
Before I wrap up, I want to share a quick pre-emptive maintenance tip that will prevent 80% of the problems I just talked about: a weekly 15-minute check. Every Friday, have your operator go through these steps: clean the feed rollers with isopropyl alcohol, inspect the punch and die for metal buildup, blow dust off all sensors with compressed air, and check the hydraulic fluid level. I’ve had customers who skipped this step and were stranded for hours waiting for a new punch, while those who did the weekly check only had minor issues that took a few minutes to fix. Busbar processing machines are built to be tough, but they still need regular care, just like any other industrial equipment.
At the end of the day, troubleshooting a busbar processing machine is about starting simple, not diving into the most complex parts first. Most problems aren’t caused by a broken motor or a faulty control panel—they’re caused by a loose wire, dirty sensor, or a roller that’s just covered in copper shavings. If you’ve walked through all these steps and still can’t figure out the issue, our team of service technicians is available 24/7 to help, whether you need a quick phone walkthrough or an on-site visit. We work with small fabrication shops and large EV manufacturers alike, so no job is too big or too small. If you’re in the market for a new busbar processing machine, or you need to replace worn parts for your current setup, don’t hesitate to reach out to our team to learn more about our equipment and service plans. We’re here to keep your production line moving, no matter what.
Busbar Inspection Machine References:
Busbar Processing Machine Operation & Maintenance Manual. Industrial Machinery Publications, 2022.
Industrial Electrical Maintenance Handbook, 5th Edition. McGraw-Hill, 2021.
Metal Stamping Troubleshooting & Best Practices. Fabricators & Manufacturers Association International, 2023.
Suzhou Kiande Electric Co., Ltd.
Suzhou Kiande Electric Co., Ltd. is one of the most professional busbar processing machine manufacturers and suppliers in China, also supports custom service and OEM&ODM service. Welcome to buy durable busbar processing machine made in China here and get quotation from our factory. Quality products and reasonable price are available.
Address: No.123, Suzhou Avenue East, Suzhou Industrial Park Suzhou, Jiangsu 215000 China
E-mail: saleswmkc@kiande.cn
WebSite: https://www.busbarcncmachine.com/
