If you’ve ever stood in a workshop watching teams work through a flange repair job that’s taking three times longer than it should, you know the frustration of dealing with misaligned, uneven flanges. As someone who’s spent the last decade supplying flange facers to workshops across industrial, oil and gas, and petrochemical sectors, I’ve seen firsthand how a well-installed machine can turn a chaotic job into a precise, efficient process. Over the years, I’ve also helped dozens of customers troubleshoot installations that went wrong before they even turned the machine on—simply because they overlooked critical setup requirements. If you’re planning to add a flange facer to your workshop, here’s the real-world breakdown of what you need to get right from the start, no cutting corners allowed. Flange Facer

First, and most non-negotiable, is the workshop floor. I can’t tell you how many times a customer has called me a week after installing their new flange facer saying the machine is vibrating so bad it’s hard to read the dials, only to find it sitting on a standard concrete workshop floor that’s not level or stable enough for the torque and forces the machine generates. Flange facers are heavy, but they also exert massive cutting forces when you’re resurfacing a 48-inch flange—enough to shift even a slightly unanchored machine if the floor isn’t up to snuff. The first rule: the floor must be a reinforced, non-expansive concrete slab with a minimum compressive strength of 3,000 psi. Wait for it to cure fully—usually 28 days for a new slab, and at least 7 days if you’re patching a damaged area—before setting anything up. I once had a customer rush installation on a 10-day-old slab, and within a month the slab sank ¼ inch under the machine’s weight, throwing all their flange alignment readings off. That cost them two full weeks of missed jobs and $12,000 in rework—all because they skipped the cure time.
Next, the floor has to be perfectly level, and I mean within 0.005 inches over a 10-foot span, not the ¼ inch most workshop levels give a pass on. The precision required for a flange facer means any tilt will result in an uneven cut, leading to leaks, extra machining time, or even reworking the entire flange. To check this, don’t just use a spirit level on the floor—place a long, straight aluminum beam across the slab, rest a precision dial level on top of the beam, and take readings every 12 inches along its length. If you find low spots, you can’t just prop the machine up with wooden blocks or shims. Use steel shims only, and make sure they’re as thin as possible, evenly spaced, and torqued down once the machine is bolted in place. Wooden shims compress over time, leading to alignment drift. For extra stability, I always recommend that customers pour a custom concrete pit or mount the machine to a heavy-duty steel base plate. The base plate should be at least 2 inches thick, cut to fit the machine’s footprint, and secured to the floor with anchor bolts rated for at least 15,000 psi tensile strength. I supply our standard base plates with every machine for this exact reason, but I’ve seen workshops use scrap steel that flexes—another recipe for cut inaccuracies.
Then there’s the critical step of assessing your available power supply. Flange facers are powerhouses, but they’re also sensitive to inconsistent voltage, which can burn out motors, cause uneven cutting speeds, or trigger safety shutdowns mid-job. The last thing you want is your machine cutting a flange 30 feet up on a pipe and the motor dies because your workshop’s power drops mid-cut. The requirements here depend on the size of your machine, but as a rule of thumb: all flange facers require a dedicated power circuit, no shared outlets with welders, air compressors, or other heavy equipment that spikes power draw. For small to medium portable flange facers (up to 24-inch flange capacity), you’ll need a 240V single-phase circuit with a minimum 30 amp breaker, and a voltage tolerance of ±5% from the machine’s rated voltage. For larger fixed or heavy-duty portable facers (24-inch and up), you’ll need 480V three-phase power, a 60 amp breaker, and ±3% voltage tolerance. I always advise customers to have an electrician do a full load test on their circuit before delivery—don’t take a visual inspection of a breaker panel as good enough. Last year, a Gulf Coast petrochemical shop tried to install a 36-inch fixed flange facer on an existing circuit that only supported a 40 amp breaker. The first time they ran a heavy cut, the breaker tripped, and the motor overheated so bad it needed a full replacement. That repair cost them $4,500, not to mention the 10-day delay for a critical flange resurfacing job.
Ventilation is another factor most first-time installers completely overlook, especially in workshops where they’re dealing with fumes from welding, painting, or chemical storage. Flange facers produce two types of hazards: fine metal shavings that can clog the machine’s internal components, and heat that can build up in enclosed or unventilated spaces. If you’re installing a fixed flange facer in an enclosed pit, you need a dedicated ventilation system that exchanges at least 6 air changes per hour, and a dust collection line connected directly to the machine’s chip chute. For portable flange facers that might be used in different parts of the workshop, a portable dust extractor rated for metal shavings is mandatory. I’ve also seen customers install flange facers in areas near flammable storage tanks or open gas lines, and the combination of metal sparks from cutting and poor ventilation creates a serious fire risk. Our machines are rated for Class I, Division 2 locations if ordered for hazardous areas, but that doesn’t mean you can skip basic ventilation rules. In fact, for any workshop, a basic ventilation setup near where flange facers are in use is a non-negotiable OSHA requirement, not just a convenience.
Now, let’s talk about space and accessibility, which ties directly to how often you’ll use your flange facer and how efficiently you can run jobs. Many workshops cram their machines into tight corners to save space, but a flange facer needs clearance on all sides to operate safely and accurately. For a fixed flange facer, you need at least 3 feet of clearance on all sides to load flanges, change cutting tools, and access the control panel. For portable flange facers, you need enough space to move the machine around pipe racks, pump units, and other workshop equipment, plus a 2-foot clearance between the machine and any power lines, gas lines, or other hazardous infrastructure. I once worked with a mid-sized refinery that installed a 20-inch portable flange facer in a corridor between two large pipe racks. Every time they tried to move the machine, they had to disassemble half their pipe support framework, which added an extra 45 minutes to every job. That not only wasted labor hours but also increased the risk of accident. Now they’ve allocated a dedicated 10×12 foot space in their fabrication bay for flange facing jobs, and their monthly job turnaround is up by 20% as a result.
Don’t forget about alignment prep for the flanges themselves, even before you get to the machine setup. A flange facer can only do so much if the pipe it’s mounted to isn’t aligned properly. Before installing the machine, you need to check the flange’s runout and face parallelism using a dial indicator. The maximum allowable runout for most industrial flanges is 0.010 inches, and parallelism is 0.005 inches. If the pipe has more runout than that, you’ll need to do preliminary alignment with jacks or shims before mounting the flange facer. I always supply a free alignment tool with every machine I sell, and I also provide a step-by-step alignment guide to help customers get this right. Last quarter, a customer tried to mount their flange facer to a pipe with 0.025 inches of runout, and after the cut, the flange leaked under hydrostatic testing. They had to rework the entire flange, which cost them $8,000 and a customer warning—all because they skipped the pre-installation pipe alignment check.
Once all the physical requirements are met, there are post-installation steps that are just as important for long-term performance. First, run a test cut on a scrap steel flange to verify the machine’s calibration. This is where precision matters most—set the machine to cut a specific depth, run it for a full cycle, and measure the resulting flange face with a micrometer to make sure it’s within tolerance. I always train my customers to do this test cut before taking on paid jobs, and I offer on-site calibration services for customers who don’t have in-house metrology expertise. Also, schedule regular maintenance checks: every 100 hours of operation, tighten all anchor bolts, inspect the cutting tools, and check the machine’s level. Every 500 hours, replace the hydraulic fluid (if applicable) and calibrate the machine’s control panel.
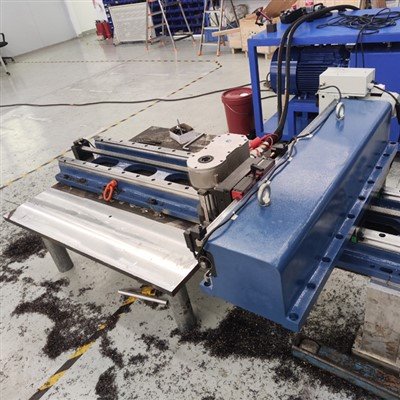
I know installation can feel overwhelming, especially if you’re adding a flange facer to an existing workshop setup. But over the years, I’ve learned that taking the time to get these installation requirements right pays off tenfold in reduced downtime, higher quality work, and longer machine life. I’ve seen too many customers buy a cheap or mismatched flange facer, then cut corners on installation, only to deal with constant breakdowns and rework that cost them far more than investing in proper setup. If you’re ready to add a flange facer to your workshop, or you have questions about whether your space meets the requirements I’ve outlined, reach out to our team for a one-on-one consultation. We’ll help you assess your workshop, recommend the right machine for your needs, and guide you through every step of installation to make sure your new flange facer works as hard as your team does.
Line Boring Accessories References
- OSHA General Industry Standards, 29 CFR Part 1910: Occupational Safety and Health Administration, Washington, D.C., 2023.
- Flange Facer Installation and Operation Manual, Industrial Machining Equipment Association, 2022.
- American Petroleum Institute (API) Standard 601: Welded Steel Tanks for Oil Storage, Third Edition, API Publishing Services, Washington, D.C., 2021.
- National Electrical Code (NEC) Article 430: Motors, Motor Circuits, and Controllers, National Fire Protection Association, Quincy, MA, 2023.
- Precision Alignment for Industrial Machinery, Third Edition, Society of Manufacturing Engineers, Dearborn, MI, 2020.
Shangqiu JDA Machinery Technology Co., Ltd.
With abundant experience, we are one of the most professional flange facer manufacturers and suppliers in China. We warmly welcome you to buy cheap flange facer for sale here from our factory. Quality products and reasonable price are available.
Address: No. 55 Pingyuan Middle Road, Liangyuan District, Shangqiu, Henan, China
E-mail: sales@jdamachines.com
WebSite: https://www.jdamachines.com/
